
Masterbatch for PE and PP Injection Molding
Injection molding grade selection begins with the polymer, mold, cycle and function of the finished part. XINYU reviews flow, filling, packing, cooling and part performance before choosing a PE filler, PP filler or moisture-control direction.
What This Application Requires
Repeatable Filling and Shot Recovery
The material must feed and plasticize consistently, pass the nozzle and gate, fill the cavity and maintain a stable cushion, cycle and part weight.
Controlled Shrinkage and Warpage
Mineral loading, flow orientation, packing, cooling and crystallization affect dimensions. Measurements must follow a defined cooling and conditioning time.
Correct Diagnosis of Surface and Internal Defects
Silver streaks, gas marks, voids, short shots and rough surfaces may involve moisture, trapped air, venting, residence time, degradation, contamination or packing.
Relevant XINYU Product Directions
PE Filler Masterbatch for Injection Molding
For selected PE molded parts where cavity filling, stiffness, dimensional response, surface, impact and cost per accepted part guide grade selection.
PP Filler Masterbatch For Injection
For selected PP molded parts where flow, screw recovery, packing, shrinkage, warpage, impact, surface and cycle economics must be confirmed on the actual mold.
Recycled PP Filler Masterbatch
For recycled PP conversion where MFR variation, mixed polymer, existing ash, degradation, filtration and the final injection, raffia or extrusion route must be reviewed together.
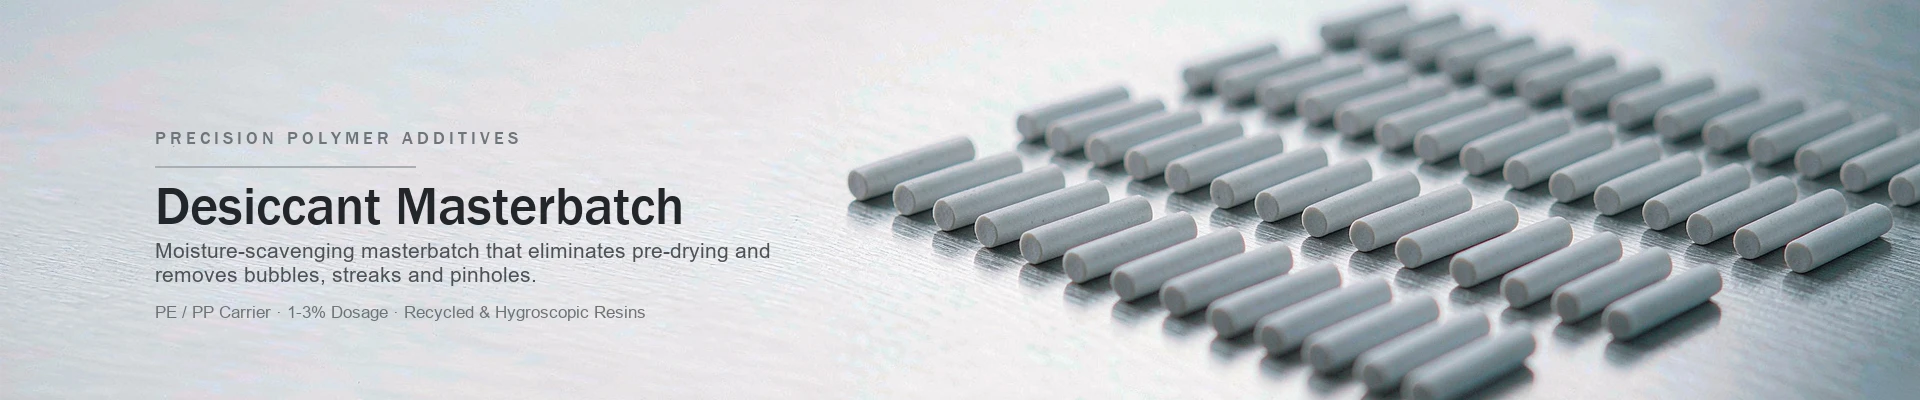
Desiccant Masterbatch for Injection Molding
For selected PE and PP injection trials where silver streaks, gas marks or voids may involve residual moisture and must be diagnosed against venting, packing and degradation.
Anti Moisture Masterbatch
A broader moisture-control direction for selected polyolefin recycling and conversion routes, used after the water path, venting, filtration and downstream defect have been mapped.
CaCO₃ Filler Masterbatch
The general selection entry for calcium-carbonate-filled PE and PP processing, used to route an inquiry by polymer, equipment, process and finished-product requirement.
What to Review During a Trial
Provide the PE or PP grade, regrind ratio, current formulation, part drawing, wall thickness, gate layout and required function.
01
Record barrel profile, screw recovery, back pressure, shot size, cushion, injection and holding response, mold temperature and cycle time.
02
Separate filling defects from cooling, ejection and material-handling defects during the comparison.
03
Approve the trial through part weight, surface, dimensions, warpage, impact, assembly and the tests required by the end use.
04
What to Share with XINYU
Send the polymer, regrind condition, mold and part information, current cycle, main defect and acceptance tests. XINYU will identify the most relevant product family and starting performance tier.
Discuss Your Molded Part
Describe the part, mold and main production constraint. We will focus the first discussion on the variables that control accepted parts per cycle.